Produttore di stampi per preforme in PET: attrezzature con punto di iniezione a otturatore da 1 a 72 impronte
Progettiamo e produciamo stampi a iniezione per preforme in PET ad alta precisione da 1 a 72 impronte per acqua minerale, bevande gassate CSD, bottiglie per olio alimentare, barattoli a bocca larga e taniche da 5 galloni. Costruiti in acciaio inossidabile Assab S136 temprato sotto vuoto (HRC 50–52) con canali caldi a punto di iniezione a otturatore pneumatico, garantendo un'eccentricità di parete ≤0,05 mm e bassi livelli di acetaldeide (AA).

- Assab S136 Stainless (HRC 50–52, 3M+ Shots)
- Punto di iniezione a otturatore pneumatico (nessun filamento al punto di iniezione)
- ≤ 0.05 mm Wall Eccentricity & ≤ 0.08g Weight Var.
- Anelli di collo intercambiabili in pressa (PCO 1881/1810)
Che cos'è uno stampo per preforme in PET?
Uno stampo per preforme in PET è uno stampo a iniezione multicavità, tipicamente da 1 a 96 cavità, che inietta resina PET fusa in cavità in acciaio raffreddate per formare una preforma a forma di provetta. La preforma viene successivamente riscaldata e soffiata per stiramento nella bottiglia finale su una macchina soffiatrice separata. La precisione dello stampo controlla direttamente l'uniformità dello spessore della parete, la nitidezza del punto di iniezione e il livello di acetaldeide (AA) nella bottiglia finita.
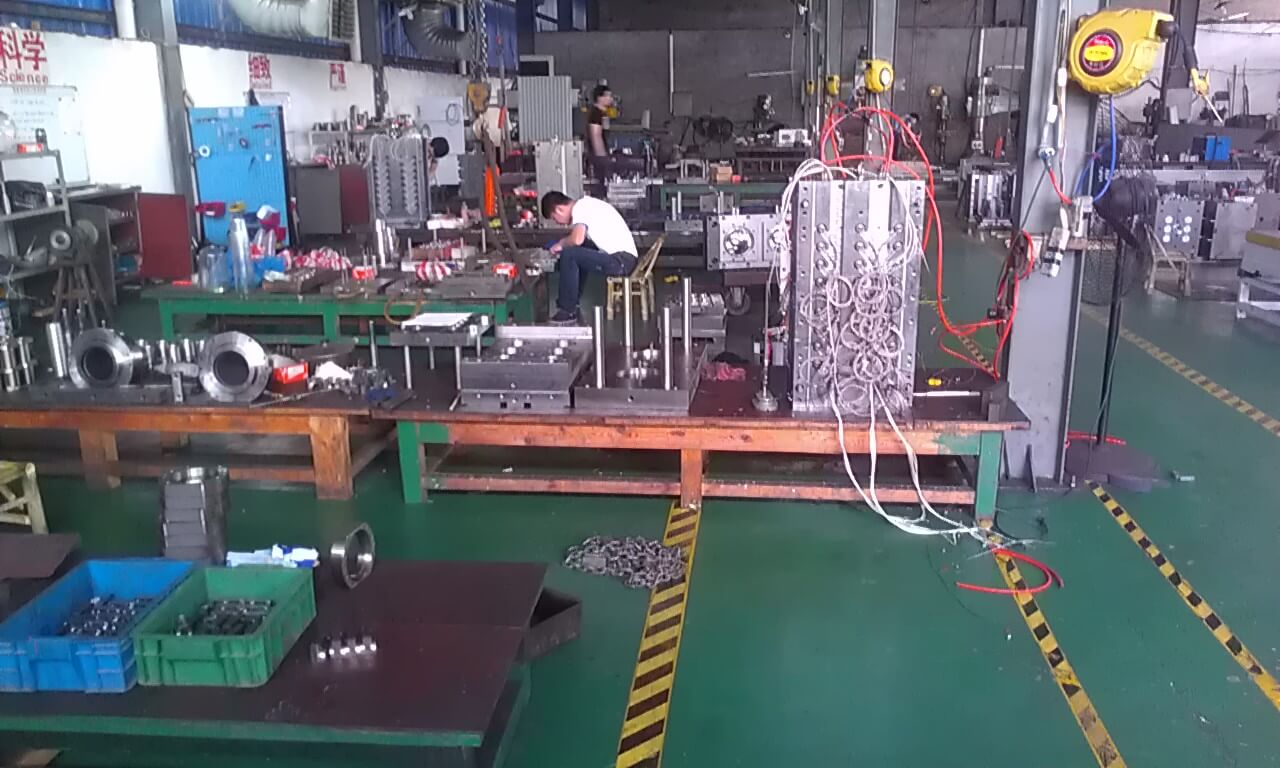
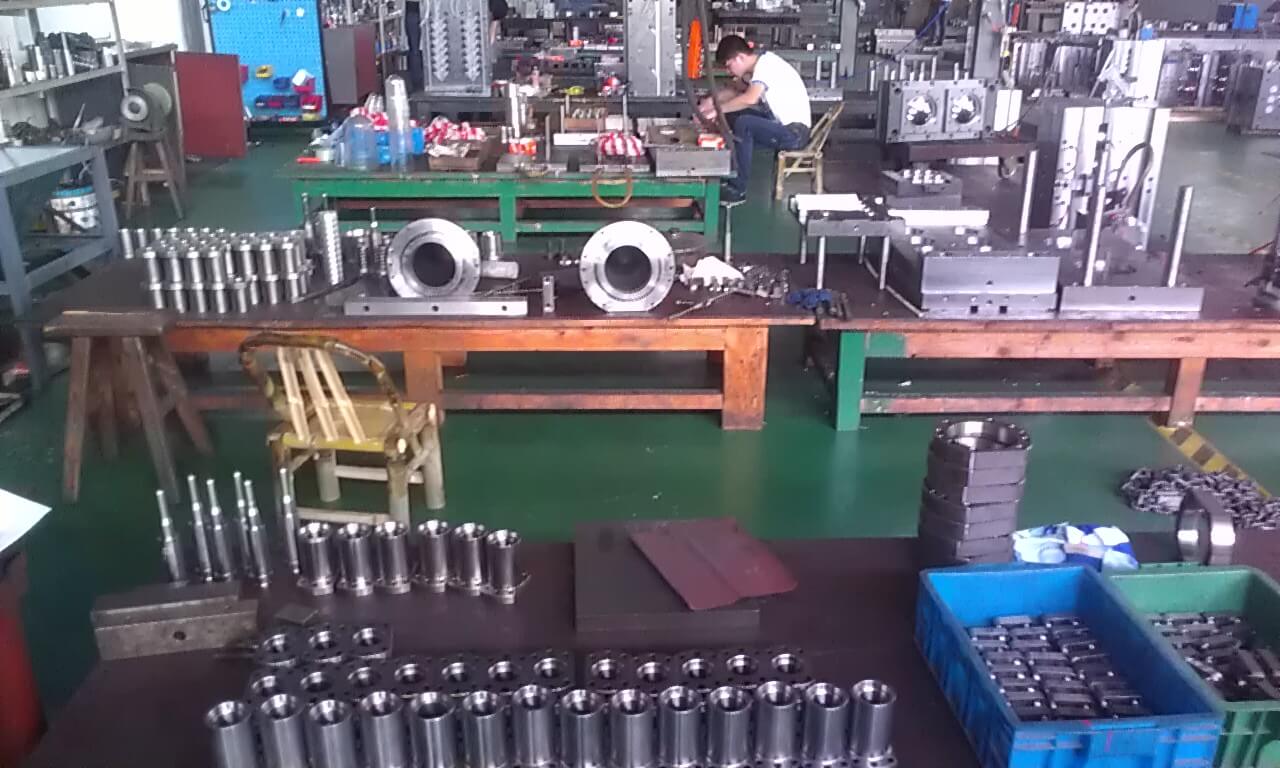
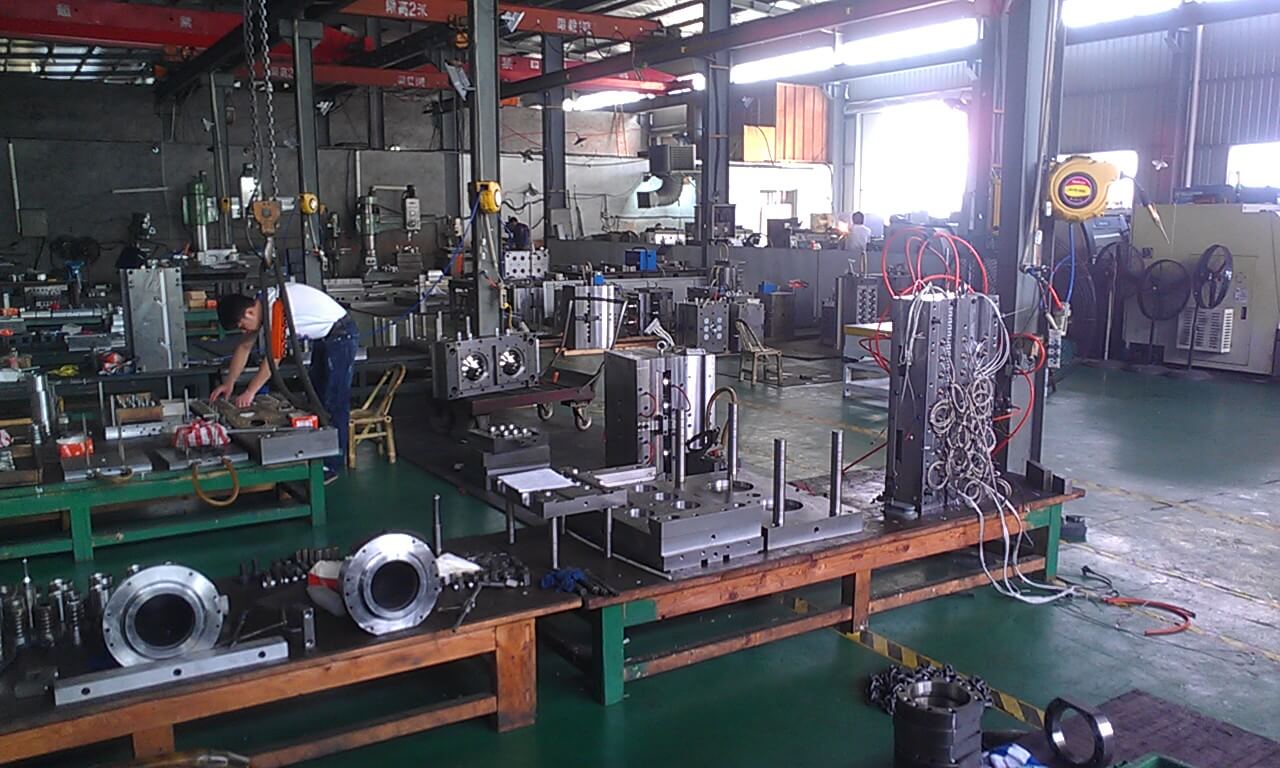

Perché gli stampi per preforme in PET di qualità inferiore compromettono la resa dello stretch-blow molding
Una bottiglia in PET è valida solo quanto la preforma da cui viene soffiata. Anche un difetto minore nello stampo per preforme provoca bottiglie che scoppiano, colli deformati o acqua con sapore alterato sulla vostra linea di stretch-blow ad alta velocità:
Cristallizzazione del punto di iniezione (opacità bianca del punto di iniezione)
Se lo spillo della valvola chiude in ritardo o il raffreddamento attorno all'inserto del punto di iniezione è insufficiente, il PET cristallizza formando una zona bianca sul fondo della preforma — causando la rottura della base della bottiglia durante lo stretch blow molding biassiale.
Eccentricità della parete della preforma (>0,10 mm)
Quando i maschi si flettono durante l'iniezione, un lato della parete della preforma risulta più spesso dell'altro. Durante lo stretch blow molding, il lato sottile si sovraestende e si rompe, mentre il lato spesso rimane madreperlaceo.
Acetaldeide (AA) elevata e variazione di peso
Dead spots or shear-heating imbalances inside a poorly machined hot-runner manifold degrade PET resin, spiking acetaldehyde (AA) levels that taint mineral water taste and creating >0.3g weight swings across cavities.
PET Preform Mould Specifications: Self-Locking vs. High-Cavitation
Every cavity, core pin, and split neck ring (lip cavity) is CNC-ground to full interchangeability tolerances (±0.005 mm):
| Parametro dello stampo | 4 to 24 Cavities (Jar / Oil / 5-Gal Preform) | 32 to 72 Cavities (High-Speed Water / CSD Preform) |
|---|---|---|
| Cavity, Core & Neck Steel | Assab S136 Stainless (Vacuum Hardened HRC 50–52) | Assab S136 (Cavity/Core) + TiN Coated H13/S136 Split Neck Rings |
| Mold Base Steel | P20 Pre-hardened + Electroless Nickel Plated Plates | 420 Stainless (1.2316) Rust-Proof Mold Base |
| Locking Architecture | Individual Self-Locking per Cavity | Individual Dual-Taper Self-Locking + Synchronized Carrier Plate |
| Sistema a canale caldo | Pneumatic Valve-Gate Manifold (PID Closed-Loop) | Naturally Balanced Rheological Manifold + Pneumatic Valve Pins |
| Wall Eccentricity | ≤ 0.06 mm (on 5-gallon / heavy preforms) | ≤ 0.04 mm (on 10g–35g beverage preforms) |
| Shot-to-Shot Weight Var. | ≤ ±0.10 g | ≤ ±0.05 g across all cavities |
| Cooling System | Spiral Core Tube + Chilled Gate Insert + Neck Ring Channels | 3-Stage Post-Mold Take-Out Cooling Plate (Optional) + BeCu Gate Caps |
| Tempo ciclo obiettivo | 18 – 28s (Edible Oil) / 38 – 55s (700g 5-Gallon) | 10 – 15 seconds (with take-out cooling) / 15 – 19s (in-mold) |
| Guaranteed Mould Life | 2,500,000+ shots | 3,000,000 – 5,000,000+ shots |
The two bands above cover our most common configurations. 1–3 cavity prototype tools and 25–31 cavity transitional layouts are quoted individually to match your press tonnage.
For a complete breakdown of cavity count calculation, hot-runner shear control, and PCO neck standards, read our Complete PET Preform Mould Buyer’s Guide.
PET Preform Neck Finishes & Applications We Tool
Water & CSD Beverage (PCO 1881 / 1810 / 26mm / 28mm)
Lightweight 9.5g to 28g water preforms and thick-neck carbonated soft drink (CSD) preforms with precision thread splits and zero parting flash on the sealing rim.
5-Gallon (18.9L / 20L) Water Carboy Preforms
4-, 6-, and 8-cavity heavy-wall (650g–800g) 55mm neck preform moulds engineered with deep spiral core cooling to prevent thick-wall crystallization haziness.
Wide-Mouth Jar, Edible Oil & Cosmetic Preforms
38mm, 48mm, 63mm, 83mm, and 110mm wide-mouth jar preforms, 3-to-5L cooking oil handle preforms, and 20/410 – 24/410 cosmetic dropper/spray preforms.
Individual Self-Locking & Zero-Stringing Valve Gates
1. Dual-Cone Individual Cavity Self-Locking
Every single cavity, core pin, and split neck ring features an independent dual-tapered self-locking cone ground on Swiss Studer cylindrical grinders to ±0.002 mm. Even on a standard toggle press, the core cannot shift — guaranteeing uniform bottle wall thickness after stretch blowing.
2. Pneumatic Valve-Gate & Low-AA Manifold
Our naturally balanced hot-runner manifold uses smooth, dead-spot-free melt channels and pneumatic cylinder valve pins that shut off cleanly inside water-cooled gate inserts — leaving a smooth <0.2 mm gate vestige with zero stringing and zero gate crystallinity.
Injection Process Parameters We Design Around
Preform quality is set as much by process window as by steel. Every mould we build is matched to these target parameters so your molder hits spec on day one:
Attrezzature per rPET e contenuto riciclato
Running 30–100% recycled PET changes melt viscosity, IV (intrinsic viscosity) drop, and contamination risk at the gate. We adjust the manifold and venting for rPET programs:
- Wider, dead-spot-free melt channels to handle the lower, more variable IV of rPET without extra shear heating.
- Extra cavity venting to clear off-gassing from recycled flake without leaving burn marks.
- Gate inserts sized to resist faster wear from any residual contamination in the recycled stream.
Complete PET Preform + Cap + Stretch-Blow Mould Package
Launching a complete bottle line? We engineer the entire tooling ecosystem under one roof so your preform neck thread, bottle cap, and blow mould fit together with 100% leak-proof torque:
- PET Preform Moulds (1 to 72 Cavities): S136 vacuum-hardened, fully interchangeable spares.
- Closure & Flip-Top Cap Moulds (8 to 48 Cavities): Consulti la nostra plastic cap & closure moulds e flip-top cap moulds.
- Stretch Blow Bottle Moulds: Aircraft-grade 7075 aluminum or S136 blow cavities — see our blow mold manufacturing.
Manutenzione ed estensione della vita utile dello stampo
A preform mould is a long-term capital asset. These are the service intervals that keep cavities within spec through their full rated shot life:
Every 250,000–500,000 Shots
Full cavity/core polish, neck-ring gauge check, and hot-runner nozzle tip inspection to catch early gate wear before it shows up as flash.
Spare Parts On Hand
Every mould ships with a spares kit (heaters, thermocouples, O-rings, neck inserts) so worn components swap on-site without machining delay.
Refurbishment & Conversion
Past the original rated life, cavities, cores, and neck rings can be re-ground and re-coated, or the mould converted to a different neck finish or gram weight, rather than re-tooling from scratch.
Sourcing a PET Preform Mould?
Send your bottle drawing, preform gram weight, neck standard (e.g., PCO 1881, 38mm, 55mm), and hourly output target. We will recommend the optimal cavity count and return an itemized quote within 24 hours.
FAQ sugli stampi per preforme PET
Come si sceglie il numero corretto di impronte (8, 16, 24, 32, 48 o 72) per uno stampo per preforme in PET?
Cavity count is matched to your stretch-blow molding machine output and injection press clamping tonnage/shot weight. For example, at a 15-second cycle, a 16-cavity mould produces ~3,800 preforms/hour, a 24-cavity mould produces ~5,700/hour, and a 48-cavity mould produces ~11,500+/hour. Share your bottle volume and press model, and we will size the exact cavitation.
Quanto costa uno stampo per preforme in PET in Cina?
An 8- or 12-cavity valve-gate PET preform mould in Assab S136 stainless steel typically ranges from USD 12,000 to USD 22,000. A 24- or 32-cavity self-locking valve-gate preform mould costs between USD 25,000 and USD 45,000, while high-speed 48- to 72-cavity systems with take-out cooling plates range from USD 50,000 to USD 88,000+.
Come si previene la cristallizzazione bianca in corrispondenza del punto di iniezione e del collo della preforma?
PET crystallizes white if it stays between 120°C and 200°C too long without rapid quenching. We surround every valve-gate nozzle tip with dedicated chilled-water channels (8–10°C) and run deep spiral cooling tubes to the very tip of the S136 core pin, quenching the gate amorphous and crystal-clear immediately after valve-pin shutoff.
I vostri cavità per preforme, maschi e anelli del collo sono intercambiabili?
Yes. All cavities, core pins, and split neck rings are CNC-ground to within ±0.005 mm tolerance and supplied with a spare-parts kit (extra heaters, thermocouples, O-rings, and neck inserts) so any worn insert can be replaced on-site without hand-fitting.
Qual è la differenza tra attrezzature per preforme in PET a una fase e a due fasi?
Two-stage (our standard scope) injects the preform, then reheats and stretch-blows it on a separate machine — it is what the specs and cavity ranges on this page cover. One-stage (injection-stretch-blow) molds and blows the bottle on one machine using a different, lower-cavitation tool; ask us separately if your line uses a one-stage system.
Con quale frequenza deve essere sottoposto a manutenzione uno stampo per preforme in PET?
We recommend a full cavity/core polish and neck-ring gauge check every 250,000 to 500,000 shots, with hot-runner nozzle tips inspected at the same interval. Logging shot count against this schedule is the single biggest factor in reaching the 2.5–5 million+ shot mould life we guarantee.