Injection Mold Cost Breakdown: Mold Base, Cavities, Steel, Slides, and Hot Runner
A buyer-focused guide to what sits inside a mold quote.
Injection Mold Cost Breakdown: Mold Base, Cavities, Steel, Slides, and Hot Runner — it all comes down to one buyer question. What are you actually paying for? A mold quote covers design, steel, machining, fitting, polishing, texture, trials, and project handling.
Most U.S. buyers look at the final number first. That’s normal. A mold can cost thousands before a single part ships. But the better question is scope, not price.
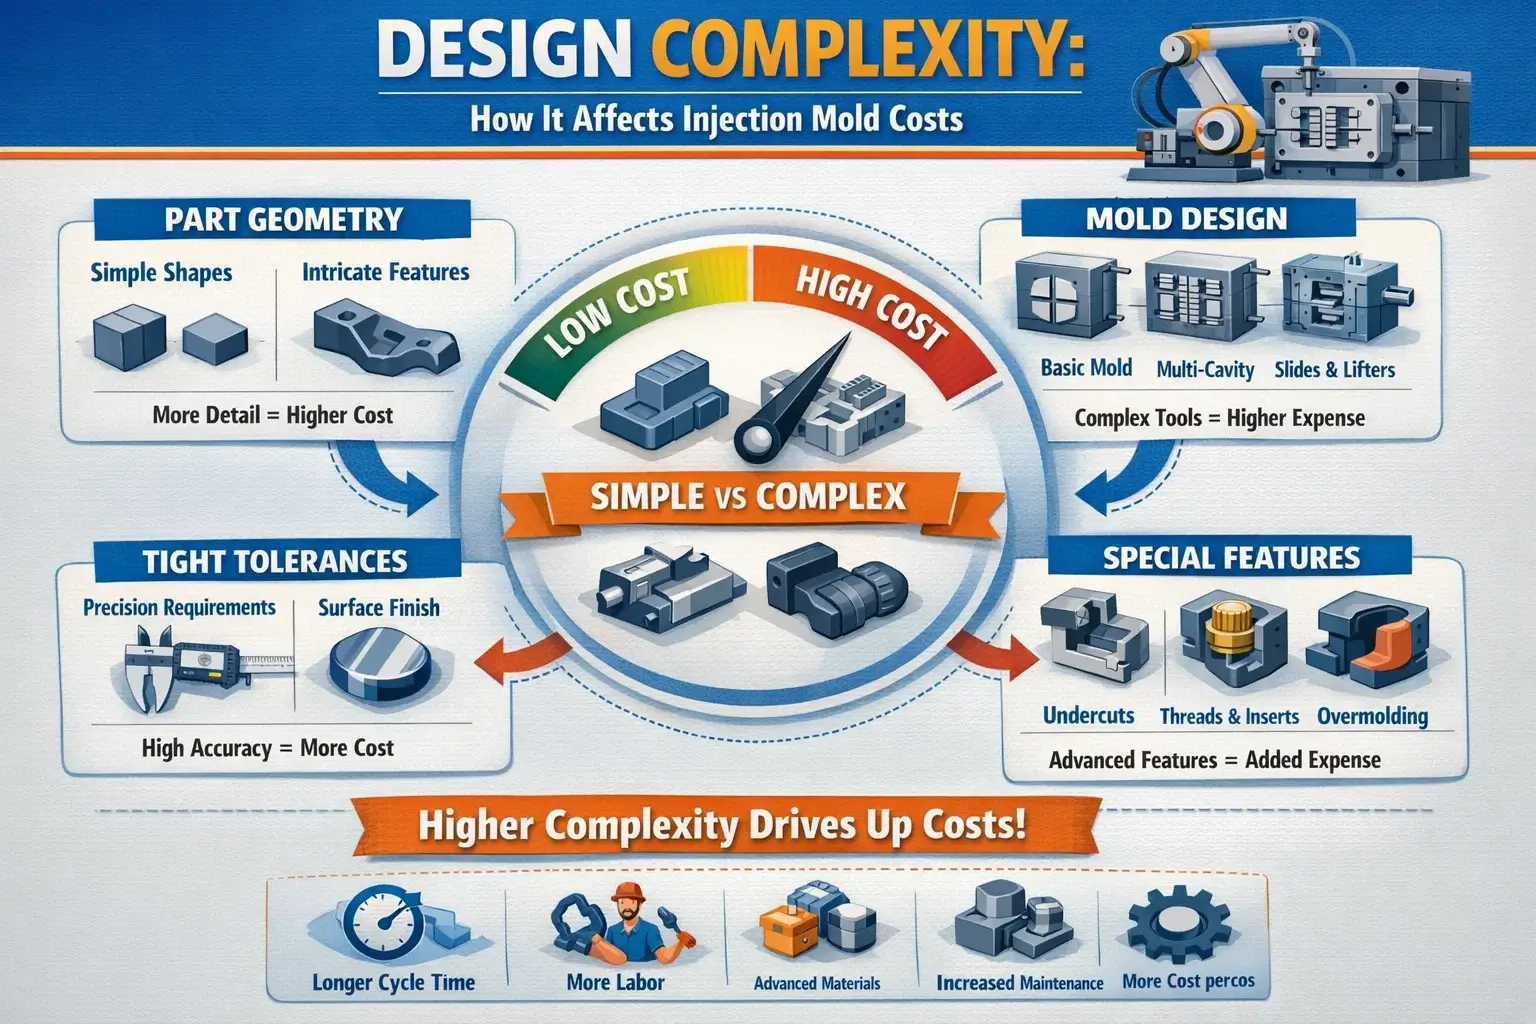
A quote reflects mold size, base type, cavity count, steel, cooling, ejection, gates, runners, and finish. It also covers slides, lifters, inserts, texture, samples, tooling standards, export packing, and documents.
A straight-pull mold runs much cheaper than one with slides and hardened steel. Mirror polish and a branded hot runner push the price up fast. This is why two suppliers quote wildly different numbers for the same part. They aren’t quoting the same mold.
Injection Mold Cost Breakdown: Mold Base, Cavities, Steel, Slides, and Hot Runner
This breakdown splits a quote into its real cost drivers. They’re structural, functional, material, and production choices. Together they explain most price gaps between suppliers.
| Cost Driver | What It Controls | Why It Affects Price |
|---|---|---|
| Mold base | Mold structure and support | Larger plates cost more and need more machining. |
| Cavities | Parts made per cycle | More cavities raise tooling cost but lower part cost at volume. |
| Steel | Tool life, polish, wear, and corrosion resistance | Better steel costs more but protects quality and mold life. |
| Slides | Side features and undercuts | Moving steel needs machining, fitting, and maintenance. |
| Hot runner | Melt delivery and runner waste | Higher upfront cost can reduce waste and labor. |
This makes comparison easier. A low quote might use softer steel, fewer cavities, or a cold runner. A higher quote might add better cooling, branded parts, and export-ready documents. Neither one is automatically right.
The right mold depends on part design, resin, volume, quality needs, and risk. I’ve watched cheap tools turn expensive after flash, sticking, and slow cycles. A clear scope protects you before you pay the deposit.
Why does the mold base affect cost?
The mold base sets cost because it holds the whole tool together. It carries the core, cavity, cooling, ejectors, guide pins, and moving parts. A weak base lets the mold move under pressure.
A mold base includes plates, guide systems, support pillars, and ejector plates. Standard bases cut engineering time because many dimensions are already fixed. DME describes mold bases and plates as pre-engineered assemblies. [VERIFY]
The base costs more when the part is large or the layout is wide. A high projected area adds cost too. So do thicker plates, higher pressure resistance, slides, or complex ejection. Buyer standards like DME, HASCO, or metric components also move the price.
A weak base causes deflection, flash, and poor parting-line control. It also wears faster. A stronger base costs more upfront but protects part quality cycle after cycle. Ask whether the base matches the resin, part size, tonnage, and volume.
How do cavities change mold cost and part price?
Each cavity adds machining, polishing, cooling, venting, and inspection. A one-cavity mold makes one part per cycle. A four-cavity mold makes four. More cavities, more build cost.
The four-cavity tool costs more to build. But it can lower part cost when demand holds steady. This isn’t only a tooling decision. It’s a production economics decision.
| Mold Type | Upfront Mold Cost | Part Cost | Best For |
|---|---|---|---|
| Single-cavity mold | Lower | Higher | Prototypes, low volume, uncertain demand |
| Two-cavity mold | Medium | Medium | Moderate volume and balanced risk |
| Four-cavity or higher | Higher | Lower | Stable demand and high annual volume |
| Family mold | Medium to high | Can be efficient | Related parts with similar size and resin |
More cavities also raise technical risk. Every cavity must fill evenly, and cooling must stay balanced. Gate size and runner layout must give repeatable parts. A high-cavity tool is smart when demand is proven. It’s risky when the product is still changing.
Why does steel selection matter so much?
Steel controls mold life, polish, wear, corrosion resistance, and repair behavior. Common picks include P20, 718, H13, S136, 420 stainless, and other tool steels. Different countries use equivalent grades under different names.
Confirm grade, hardness, heat treatment, and certificate needs. The right steel depends on resin, filler content, surface needs, volume, corrosion risk, polish, and maintenance plan.
Glass-filled nylon wears steel faster than polypropylene. PVC and flame-retardant resins often need corrosion-resistant steel. Optical or glossy parts need steel that polishes well. Uddeholm notes that molding steels may need corrosion resistance, wear resistance, polishability, and toughness. [VERIFY]
Cheap steel lowers the mold price. It also raises the risk of wear, rust, flash, and repair bills. For U.S. buyers, the steel must be named. “Good steel” is not a spec.
- Steel grade
- Steel hardness
- Core and cavity steel
- Slide steel
- Insert steel
- Heat treatment plan
- Steel certificate availability
- Expected mold life
When do slides increase mold cost?
Slides add cost when the part has undercuts or side features. Side holes, windows, clips, hooks, and threads block straight ejection. A straight-pull mold opens one way, and the part ejects without side motion.
When a side feature locks the part, the tool needs another path. That might be a slide, lifter, collapsible core, insert, or a redesign. Protolabs explains that side actions mold undercut geometry in non-straight-pull molds. [VERIFY]
A slide isn’t one part. It’s a slide core, angle pin, wear plates, guide blocks, locking blocks, and limit mechanisms. It adds fitting, spotting, and maintenance risk too. That’s why one small side hole can move a quote more than buyers expect.
Slides also grow the mold. They need travel space, support, and clean shut-off faces. One side hole may need one slide. Four side windows may need four. A threaded cap may need unscrewing, not a normal slide.
Is a hot runner worth the extra cost?
A hot runner is worth it when volume, waste, cycle time, or cosmetics justify the spend. A cold runner lets plastic freeze in the runner. That runner ejects with the part. It may need trimming, regrind, or disposal.
A hot runner keeps resin molten in heated channels. It delivers melt closer to the cavity. Hot runners cost more to build and maintain. They cut runner waste in high-volume production. Xometry describes hot runners as costlier to set up and maintain than cold runners. [VERIFY]
| Question | Cold Runner May Fit | Hot Runner May Fit |
|---|---|---|
| Is annual volume low? | Yes | Usually no |
| Is resin expensive? | Maybe | Often yes |
| Is runner waste large? | Maybe | Yes |
| Is the part cosmetic? | Maybe | Often yes |
| Is the mold multi-cavity? | Maybe | Often yes |
| Is maintenance support limited? | Yes | Maybe no |
| Is the resin heat-sensitive? | Often safer | Needs careful review |
A hot runner is not always better. It adds heaters, thermocouples, controllers, wiring, manifolds, nozzles, and service work. Ask for the hot runner brand, gate type, controller scope, spare parts, resin fit, and U.S. maintenance support.
How does part size affect mold cost?
Bigger parts need bigger steel, bases, machines, and support. A small electronics housing fits a compact mold. A large automotive trim panel needs a heavy base, deep ribs, long flow paths, and stronger cooling.
The mold gets heavier and harder to machine. It costs more to handle and ship. A large projected area also drives up injection pressure and tonnage. More area means more force during injection.
The mold must resist opening pressure. A weak structure deflects. Send accurate 3D files and resin data before you ask for a firm quote. Without part size, resin, wall thickness, and volume, any price is a rough guess.
How does part complexity affect cost?
Every feature must be formed, cooled, vented, ejected, and inspected. Complexity drives cost. Hard features include deep ribs, tall bosses, snap fits, thin walls, side holes, internal threads, and shut-off geometry.
Fine texture, high-gloss surfaces, insert molding, overmolding, and tight cosmetic faces add work too. Complexity eats engineering time. It also adds CNC, EDM, polishing, assembly, and trial hours.
A part can look simple outside and cost a lot inside the mold. Internal clips, screw bosses, ribs, and side ports add real tooling work. Good DFM doesn’t make a part cheap. It makes the part manufacturable.
What is deflection, and why should buyers care?
Deflection is mold steel moving under injection pressure, clamp force, or heat. It matters because it causes flash, mismatch, size variation, and early wear. A mold can look strong and still move under pressure.
Thin plates, weak supports, and high cavity pressure raise that risk. It shows up in cavity plates, core plates, slides, and long cores. It also shows in thin shut-off areas, large unsupported surfaces, and ejector systems.
Steel movement opens small gaps, and gaps cause flash. Flash means trimming work and quality complaints. Repeated movement wears shut-off surfaces and parting lines. Good design fights deflection with plate thickness, support pillars, locks, steel choice, clamp tonnage, and cooling.
Deflection rarely shows up as a quote line. But it’s baked into mold design quality. A very cheap quote may cut steel, support, or fitting time.
How do tolerances affect the tool price?
Tight limits need better machining, fitting, process control, and validation. So they cost more. A housing tolerance is not a gear tolerance. A sealing surface is not a hidden rib. Spend precision where the part needs it.
Tight tolerances can need precision CNC, EDM finishing, jig grinding, and mold flow review. They can also need steel-safe tooling, sampling rounds, CMM inspection, and process studies. These are real costs, not paperwork.
Tolerances are not only a mold issue. Shrinkage, fiber direction, cooling, gate location, and packing pressure all affect size. Define critical dimensions early. Don’t apply tight tolerances everywhere.
A good print sorts dimensions: critical-to-function, cosmetic, assembly, reference, and non-critical. This lets the mold maker spend money where it matters.
How does expected production volume affect mold cost?
The mold must match its production life. So volume drives the build. A prototype mold may use softer steel, simpler cooling, fewer cavities, or hand-loaded inserts. A production mold may need hardened steel, automated actions, full cooling, replaceable inserts, and stronger parts.
A low-volume mold is cheaper upfront. But it may not survive high-volume runs. A high-volume mold costs more now. It can cut downtime and maintenance later.
Share your annual volume, lifetime volume, launch schedule, resin, and colors. Share production location, automation needs, and spare-part requirements too. A quote for 5,000 parts a year should not match one for 1,000,000.
What quote details should U.S. buyers compare?
Compare scope before you compare the final price. A complete quote makes risk visible. A vague quote hides it. Most quote problems start when buyer and supplier assume different mold standards.
- Is the mold single-cavity or multi-cavity?
- What steel is used for core and cavity?
- Is the steel pre-hardened or fully hardened?
- What is the mold life?
- Is the mold base standard or custom?
- Does the quote include slides or lifters?
- Is the runner cold or hot?
- If hot runner, what brand?
- Is texture included?
- Is polishing included?
- Are samples included?
- Is mold trial included?
- Is inspection included?
- Are design changes included or excluded?
- Is export packaging included?
- Are 2D drawings and 3D mold files included?
- Are spare parts included?
- Is the mold built to U.S. press specifications?
Cost driver comparison table
The best mold depends on volume, resin, tolerance, part design, and business risk. Use this table to spot what a lower quote leaves out.
| Decision Area | Lower-Cost Choice | Higher-Cost Choice | Buyer Risk If Under-Specified |
|---|---|---|---|
| Mold base | Smaller, lighter base | Larger, stronger base | Deflection, flash, poor mold life |
| Cavities | One cavity | Multiple cavities | Higher part cost if demand grows |
| Steel | P20 or similar | Hardened or stainless steel | Wear, rust, poor polish, early repair |
| Slides | Redesign to avoid slides | Add slides or lifters | Part cannot eject if undercut remains |
| Runner | Cold runner | Hot runner | Waste, longer cycle, trimming labor |
| Cooling | Basic channels | Optimized cooling | Warpage, long cycle time |
| Finish | Basic polish | High polish or texture | Cosmetic mismatch |
| Tolerance | General tolerance | Tight tolerance validation | Assembly problems or high inspection cost |
How can buyers reduce mold cost without hurting quality?
Simplify the part before the tool build. Confirm volume, drop needless tolerances, and finish DFM before cutting steel. This protects cost without weakening the part.
Remove avoidable undercuts. Add proper draft angle. Keep wall thickness even, and skip unneeded deep ribs. Use standard shut-off angles, lock the resin early, and don’t switch resin after mold design.
Set cavity count by real demand. Use a cold runner for low volume when waste is acceptable. Use a hot runner only when the production math supports it. Define cosmetic areas, tighten only critical dimensions, and ask for steel-safe areas when sizes are uncertain.
The cheapest mold is not the lowest-cost mold. A tool that needs constant repair can cost more than a better-built one. Scrap, downtime, and missed deliveries erase a low quote fast.
What red flags appear in very cheap mold quotes?
Cheap mold quotes often hide missing details, weak construction, or risky assumptions. A low price can be fine for a simple low-volume tool. But the quote must spell out what’s included.
- No steel grade listed
- No mold life listed
- No cavity count listed
- No runner type listed
- No hot runner brand listed
- No mention of slides despite undercuts
- No sample plan
- No mold trial plan
- No DFM feedback
- No tolerance review
- No export standard
- No spare parts
- No documentation
- No clear payment milestone
- No change-order policy
For U.S. buyers, clear communication matters. If a supplier can’t explain scope before the order, problems get worse later. If they can’t answer basic tooling questions, that’s your answer.
FAQs
Why do two injection mold quotes for the same part differ so much?
Is a single-cavity mold always cheaper?
Does a hot runner always reduce total cost?
What steel is best for injection molds?
How do slides affect mold maintenance?
What is the difference between mold cost and part cost?
Should U.S. buyers choose a China mold supplier or a local U.S. mold maker?
Can design changes after mold build increase cost?
Conclusion
Injection Mold Cost Breakdown: Mold Base, Cavities, Steel, Slides, and Hot Runner helps you read a quote right. A mold price is not just a number. It reflects design choices, production goals, steel, complexity, and long-term risk.
Mold base strength drives deflection and tool life. Cavities drive production economics. Steel drives wear, polish, and repair risk. Slides drive fitting, maintenance, and mold size. Hot runners drive waste, cycle time, and upfront spend.
For U.S. buyers, the goal isn’t the cheapest mold. It’s the right mold for the part, resin, tolerance, volume, and quality target. A clear quote protects both sides. It cuts surprises and turns tooling money into stable production.