
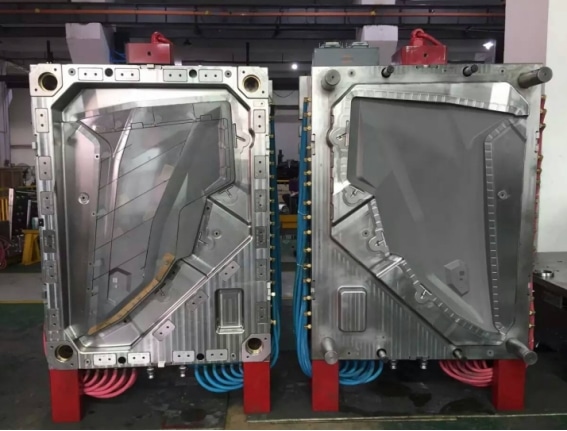
Die casting forces molten metal into a steel die under high pressure. The metal fills the cavity in milliseconds and freezes quickly against the water-cooled die walls. This process suits high production of quality parts with tight tolerances and good surface finish. This guide covers the process, machine types, alloys, design rules, and common defects.
Key takeaways
- Die casting injects molten metal into steel dies at high speed and pressure.
- Hot-chamber machines suit zinc and magnesium; cold-chamber machines suit aluminum.
- Rapid freezing gives a fine surface grain but can trap slight internal porosity.
- Uniform thin walls, draft, and generous radii are the core design rules.
- Zinc plates easily; aluminum needs more surface preparation before plating.
How die casting works
Each cycle starts with the two die halves clamped shut under high tonnage. A shot of molten metal enters the shot sleeve, and a plunger drives it into the cavity at high velocity. Intensification pressure then squeezes the metal during freezing to reduce shrinkage porosity. After a short cooling time, the die opens and ejector pins push the casting out. Operators spray die lubricant before the next shot to control die temperature and help release.
Cycle times run from a few seconds for small zinc parts to over a minute for large aluminum castings. Most machines handle at least 100 shots per hour on small parts. Large parts run slower because filling, solidification, and ejection all take longer.
Hot-chamber vs cold-chamber machines
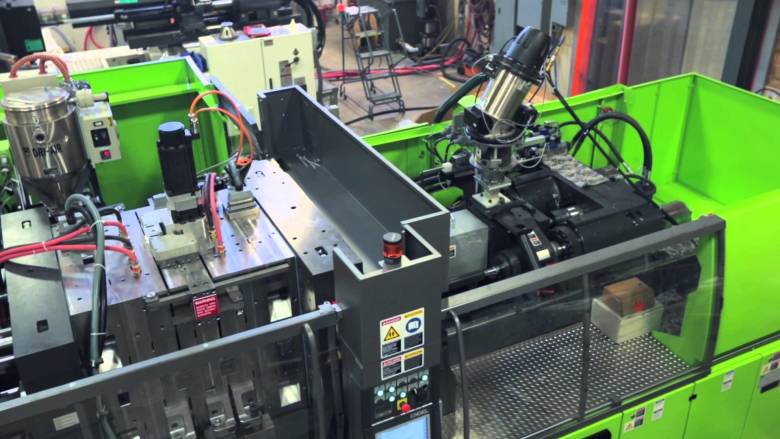
The two machine families differ in how metal reaches the shot sleeve. Hot-chamber machines keep the injection mechanism immersed in the molten metal furnace. Each shot draws metal directly, so cycles run fast. This design suits low-melting alloys such as zinc, magnesium, and tin-lead. Cold-chamber machines ladle molten metal into the shot sleeve for every cycle. The furnace stays separate, which protects the injection parts from high-melting aluminum and copper alloys. Cold-chamber cycles run slower because of the ladling step.
| Feature | Hot-chamber | Cold-chamber |
|---|---|---|
| Metal delivery | Injection unit immersed in melt | Metal ladled into shot sleeve each cycle |
| Typical alloys | Zinc, magnesium, tin, lead | Aluminum, magnesium, copper-base |
| Cycle speed | Faster | Slower |
| Machine wear | Lower with low-melting alloys | Higher, handles hotter melts |
| Shot size range | Small to medium | Medium to very large |
Materials
Most die castings use zinc, aluminum, or magnesium. Copper-base alloys, lead, and tin cover smaller niches. Zinc alloys such as Zamak 3 cast at around 420°C and give the best dimensional stability. They also take electroplating readily without special pretreatment. Aluminum alloys such as A380 and ADC12 dominate automotive parts. They offer a strong stiffness-to-weight ratio but need higher melting temperatures near 660°C. Magnesium alloys such as AZ91D are the lightest structural option. They require protective cover gas or vacuum handling because molten magnesium can ignite. Copper-base alloys wear dies faster because of their high melting points, which raises part cost.
| Alloy family | Example grades | Melting point | Key advantage |
|---|---|---|---|
| Zinc | Zamak 3, Zamak 5 | ~420°C | Tightest tolerances, easy plating |
| Aluminum | A380, ADC12 | ~660°C | Light, stiff, corrosion resistant |
| Magnesium | AZ91D | ~650°C | Lightest structural metal |
| Copper-base | Brass C85700 | ~900°C and up | High strength, wear resistance |
Mechanical properties and porosity
The mechanical properties of die castings run slightly below wrought or sand-cast equivalents. Rapid freezing in steel dies traps tiny gas pores inside the casting. This slight porosity lowers elongation and fatigue strength. Designers compensate with slightly larger safety factors on highly loaded features. The outer skin tells a different story. Fast cooling forms a fine-grained surface layer with excellent hardness and finish. Many die castings serve in applications needing reasonably high mechanical strength despite the internal porosity.
Design features
The complexity of design faces one hard limit: the part must leave a solid steel die. Undercuts and cross holes need slides or lifters, which raise tooling cost. Designers add such mechanisms only when the savings in secondary machining justify them.
- Keep wall thickness uniform and below about 1 inch. Thick sections develop internal shrinkage porosity as they freeze last.
- Small parts can go as thin as 0.025 inch in zinc. Larger parts and aluminum need thicker minimum walls.
- Add draft of at least 0.005 inch per inch for zinc. Copper-base alloys need around 0.020 inch per inch. More draft always ejects more reliably.
- Use generous fillets instead of sharp internal corners. Sharp corners concentrate stress and crack during ejection.
- Place the parting line where slight flash will not hurt function or appearance.
- Hold critical dimensions across the parting line looser than dimensions within one die half. Die halves shift slightly under clamp and thermal load.
Large masses of metal are not good in die castings; section thickness should stay below 1 inch. Tolerances can be remarkably tight. Zinc holds about ±0.001 inch per inch of length under good control. Aluminum and magnesium need somewhat wider limits. Surface finish from polished dies reaches about 60 microinches rms. Typical production runs 100 to 125 microinches, so machining is seldom necessary.
Common defects and causes
| Defect | Appearance | Typical cause |
|---|---|---|
| Gas porosity | Round internal voids | Air entrapment, poor venting |
| Shrinkage porosity | Jagged internal voids | Thick sections, low intensification |
| Cold shut | Visible seam, weak bond | Low metal temperature, slow fill |
| Soldering | Metal sticks to die | High die temperature, low draft |
| Flash | Thin fins at parting line | Worn dies, excessive pressure |
| Misrun | Incomplete fill | Cold metal, blocked vents |
FAQ
How is die casting different from injection molding?
Die casting injects molten metal into steel dies; injection molding injects plastic melt into similar tooling. Both are high-pressure, high-volume processes. Compare with the injection molding process for the plastics side.
Which alloy should I choose?
Zinc gives the tightest tolerances and easiest plating. Aluminum gives the best strength-to-weight value for larger parts. Magnesium is lightest but needs careful handling.
Can die castings be welded or heat treated?
Fusion welding is difficult because trapped gas expands and blisters the surface. Standard solution heat treatment can also blister parts. Design around as-cast properties where possible.
Why do die castings sometimes leak under pressure?
Interconnected porosity creates leak paths through thin walls. Higher intensification pressure and vacuum-assisted venting reduce the risk.
What wall thickness works best?
Keep walls uniform and under 1 inch. Small zinc parts can reach 0.025 inch. Avoid isolated thick bosses; core them out instead.
Discussing your project
Topworks Plastic Mold was founded in 2006. The company is headquartered in Huangyan, Taizhou, Zhejiang, and operates a manufacturing plant in Guangdong. Send your 3D files for a DFM review. Our engineers compare die casting with injection molding where both fit. You receive a detailed mold quote within 24 hours.