Blow Molding: Process, Types, Part Design & Applications
Blow molding shapes hollow plastic parts by inflating a heated tube of plastic against a mold cavity. It is how bottles, tanks, toys, ducts and countless hollow goods are made. This guide covers the three process types, the design rules that decide part quality, and where blow molding beats injection molding.

- Extrusion, injection & stretch blow molding
- Low tooling cost, fast cycles
- Blow-up ratio kept under 5:1
- Bottles, tanks, ducts, toys & more
What is blow molding?
Blow molding is the process used to make hollow plastic parts. A heated tube of plastic — the parison — is enclosed in a mold and inflated with air until it takes the shape of the cavity, then cooled and released.
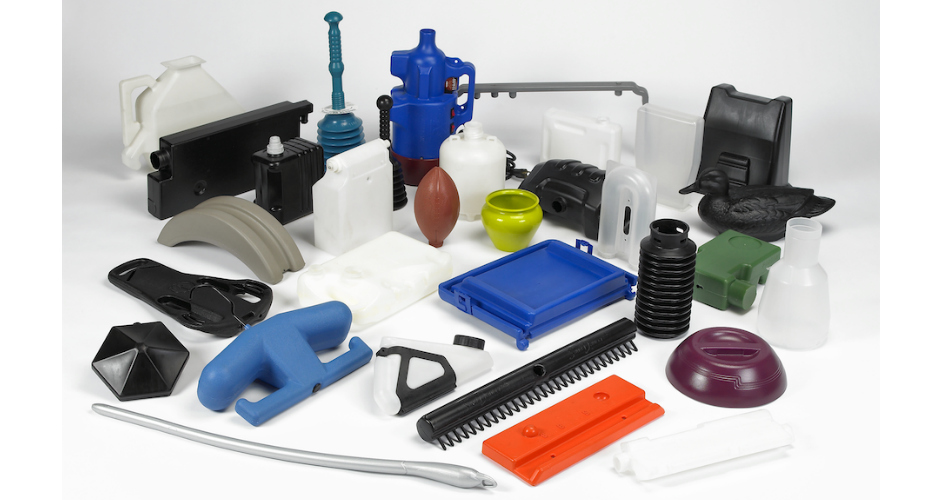
It is widely used across the toy, household, chemical, cosmetics and food industries. Typical blow-moulded products include toy cars, teapots, toolboxes, wheels, mineral-water bottles, lampshades, pots, barrels and cans, pipeline and automotive conduit, hoses, containers, depot equipment and stadium seating.
The three types of blow molding
Extrusion blow molding
A parison is continuously extruded and clamped in the mold, then inflated. The workhorse for bottles, containers, tanks and large industrial hollow parts. Lowest tooling cost.
Injection blow molding
A preform is injection-moulded first, then blown. Higher precision and a cleaner neck finish — used for smaller, higher-quality bottles and jars.
Stretch blow molding
The preform is stretched as it is blown, aligning the polymer. Standard for PET bottles — it raises tensile strength, clarity and barrier while using less material.
Applications
Blow molding suits almost any hollow part. Common categories include:
Packaging
Mineral-water and beverage bottles, chemical and cosmetic containers, barrels, cans and jars.
Industrial & automotive
Tanks, pipeline and automotive conduit, hoses, ducts, depot equipment and stadium seating.
Consumer & toys
Toy cars, wheels, teapots, toolboxes, pots and lampshades.
Novelty items
Display pieces and specialty hollow goods where a one-piece moulded shape avoids assembly.
Advantages and limitations
| Advantages | Limitations |
|---|---|
| Low mold and die cost versus injection molding | Restricted to hollow parts |
| Fast production rates | Wall thickness is harder to control |
| Can mould complex one-piece hollow shapes | Non-uniform walls if the design stretches unevenly |
| Produces recyclable parts | — |
| Stretch blow raises strength, clarity and barrier while cutting weight | — |
The process also handles high-molecular-weight polymers well, because the extrusion step is not limited the way injection is. Injection relies on lower-molecular-weight, lower-viscosity material, which reduces toughness and stress-crack resistance — so blow molding can deliver tougher hollow parts than injection molding for the same geometry.

Blow-moulded part design
A handful of standard rules prevent most blow-molding problems. The single most important one is controlling how far the plastic has to stretch.
Keep the blow-up ratio low
The blow-up ratio is the relation of maximum part diameter to the diameter of the extruded parison. Observe a maximum of 5:1, and where possible keep all work within 3:1. An improper parison-to-part ratio forces excess material to satisfy minimum wall thickness, and parts that demand excessive blow-up cool slowly in the heavy areas — giving both non-uniform walls and slow cycles.
Uniform wall thickness
Uniform walls are one of the hardest goals in the process, because the parison thins where it stretches most. For containers, the parison must be no larger than the neck to prevent neck pinch-off scars. Shapes like a pyramid or cone usually come out lighter by injection blowing than by extrusion blowing.
Choose the right blow method
Applications that do not need optimum stress-crack resistance may suit injection blowing, which gives more uniform walls and reduced weight. Where toughness and barrier matter most, extrusion or stretch blow molding is the better route. The design and the performance requirement decide the method — not the other way round.

Need a blow-moulded product made?
Send your part or bottle drawing and target volume. We’ll advise on the right blow-molding method, materials and tooling, and quote the job.
- Extrusion, injection and stretch blow molding
- Design support on wall thickness and blow-up ratio
- China-based tooling and production
Blow molding FAQ
What is blow molding?
Blow molding is a process for making hollow plastic parts. A heated tube of plastic (a parison, or a preform in injection blow molding) is placed in a mold and inflated with air until it takes the shape of the cavity, then cooled and ejected. It is how bottles, containers, tanks and many hollow industrial parts are made.
What are the main types of blow molding?
Three: extrusion blow molding (a continuously extruded parison, used for bottles, containers and industrial parts), injection blow molding (a preform is injection-moulded then blown, for higher precision and smaller bottles), and stretch blow molding (the preform is stretched and blown, used for PET bottles to improve strength, clarity and barrier while using less material).
What is the blow-up ratio, and what is the recommended maximum?
The blow-up ratio is the relation of the maximum part diameter to the diameter of the extruded parison. A maximum of 5:1 should be observed, and where possible the design should stay within 3:1. Too high a ratio gives non-uniform walls, excess material use and slow cycles from cooling heavy areas.
What are the advantages of blow molding versus injection molding?
Lower mold and tooling cost, fast production rates, the ability to mould complex hollow parts in one piece, and recyclable output. Stretch blow molding in particular makes a container from less raw material with improved strength, clarity and barrier properties. The main limitation is that blow molding is restricted to hollow parts, and wall thickness is harder to control.
Why is uniform wall thickness hard in blow molding?
Because the parison stretches unevenly as it inflates — areas that expand more end up thinner. Designers control this by keeping the blow-up ratio low, avoiding shapes that demand excessive stretch, and choosing between extrusion and injection blow molding based on the part. Uniform walls are one of the hardest goals in the process.
What products are made by blow molding?
Bottles for water and beverages, chemical and cosmetic containers, toys and novelty items, toolboxes, barrels and cans, lampshades, automotive ducts and conduit, hoses, tanks, stadium seating and many other hollow household and industrial goods.
