Insert Moulding: Metal Inserts in Injection-Molded Parts
Insert moulding embeds metal parts — usually threaded bushings — into plastic during the injection process. It replaces slow unwinding at the press with straight-draw ejection, and gives threads far stronger than molded plastic. Here is how inserts are held, when to use them, and the design rules that stop cracking.

- Threaded metal inserts
- Straight-draw ejection, no unwinding
- Cross-knurl retention
- Correct wall to prevent cracking
What is insert moulding
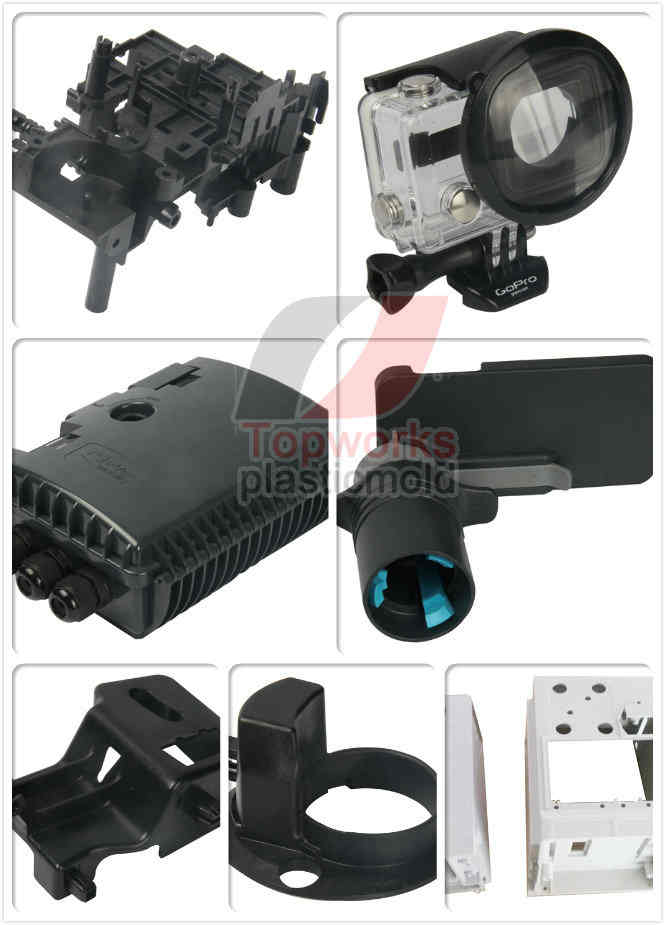
A large share of molded work uses metal insert moulding, usually specified when threaded parts are required.
By using inserts, the need for any unwinding at the press is removed and the straight-draw method of ejection can be used. During molding the inserts are embedded in the material and held by the specially cut cross-knurl on the outside of the insert. Small pins in the mould position each insert, over which the threaded piece is placed.
Metal insert vs molded thread
Whether to use an insert or mold the thread into the part itself is sometimes optional. The trade-offs are clear:
Metal insert
- Straight-draw ejection, no lengthy unwinding — saves labour
- Stronger than a molded thread; almost never strips
- Permits unlimited screwing and unscrewing
- Adds material cost, offset by labour saving
Molded thread
- Lower material cost
- Fine for large-diameter or cosmetic threads (e.g. a jar)
- Rarely strips, but repeated use is questionable
- Needs an unwinding step at the press
Diameter is the deciding factor: for small diameters or minute, deep threads, metal inserts should always be used. See related parts we mould at plasticmoulds.net.
Placing inserts in the mould
It is much more advantageous to build the mould so inserts sit in the cavity — there they are held on the pins by gravity.
Where inserts have to be placed in the top half of the die, the pins are given a slight taper so the insert holds by a wedge action when tapped lightly. Placing inserts in the force (moving) side is more arduous, but the design of the part sometimes makes it necessary. Colour of the surrounding plastic is set by the resin and any pigment added.
Enough material around the insert
Have a part that needs metal inserts?
Send the part and insert details — we’ll advise on placement, wall thickness and tooling, and quote it.
- Threaded and custom metal inserts
- Straight-draw tooling design
- DFM to prevent cracking
Insert moulding FAQ
What is insert molding?
Insert molding embeds a component — most often a metal part such as a threaded bushing — into a plastic part during the injection process. The molten plastic flows around the insert and locks it in place, usually with the help of a cross-knurl on the insert’s surface.
Why use a metal threaded insert instead of a molded thread?
A metal insert lets you use a straight-draw ejection method with no unwinding at the press, saving labour. It also surpasses a molded thread in strength, almost never strips, and permits unlimited screwing and unscrewing — something a molded plastic thread does not always tolerate.
When should I choose a molded thread over an insert?
It is often optional, and thread diameter decides. Large-diameter or cosmetic threads (a threaded jar) suit a molded thread; small diameters or minute, deep threads should always use a metal insert because a molded thread would be too weak or impractical.
How are inserts held in place during molding?
Small pins in the mold locate the insert. It is best to place inserts in the cavity, where gravity holds them on the pins. When they must sit in the top half of the tool, the pins are given a slight taper so the insert holds by a light wedge action.
How much plastic should surround an insert?
Enough to avoid cracking. Plastics and metals have different coefficients of expansion, so a minimum wall of about 1/4 inch (adding ~1/4″ around the insert) is specified to stop the material cracking out around the metal.