Automotive Bumper Mould Maker: Internal Parting & SVG Class-A Tooling
We engineer and manufacture large injection moulds for front and rear car bumpers, radiator grilles, and lower valence panels. Built in pre-hardened DIN 1.2738 / 718H steel with Internal Parting technology and 8-to-12 drop Sequential Valve Gate (SVG) hot runners, achieving 40–55s cycle times on 1,800T–3,200T presses with zero weld lines on Class-A painted surfaces.

- Internal Parting (Hidden Seam Lines)
- 8–12 Drop SVG Sequential Hot Runner
- DIN 1.2738 / 718H + Nitrided Lifters
- 500,000–1,000,000+ Shot Tool Life
Why Car Bumper Moulds Fail Without Upfront Engineering
A front or rear bumper fascia is one of the largest, most complex thin-wall parts on a vehicle (typically 1,800–2,200 mm wide with a 2.5–3.2 mm wall). Three tooling mistakes account for 90% of bumper production failures:
Parting-Line Flash on Class-A Surfaces
Traditional external parting leaves a witness seam along the wheel-arch flange and fog-light bezel. After 50,000 shots, flash requires manual knife trimming before painting. We solve this with Internal Parting technology that hides the split line on the inner non-visible lip.
Weld Lines & Flow Marks
Simultaneous multi-gate injection traps air where melt fronts collide, leaving visible knit lines across the bumper face. We use Sequential Valve Gating (SVG) triggered by hydraulic/pneumatic cylinders so a single continuous melt wave sweeps across the part.
Post-Mold Warpage & Wing Splay
Modified PP+EPDM-TD20 shrinks anisotropically (0.9%–1.3%), causing the two wraparound fender wings to bow inward or outward after ejection. We apply Moldflow pre-deformation compensation directly into the 5-axis CNC toolpath so the cooled part springs into exact car-body gauge tolerance.
Automotive Bumper Mould Specifications: Aftermarket vs. OEM Tier-1
Whether you are tooling a replacement aftermarket bumper line (AM) or an OEM Tier-1 passenger vehicle program, we size the steel, runner, and mechanism to match your target volume and capex:
| Tooling Parameter | Aftermarket (AM) Bumper Mould | OEM Tier-1 Production Bumper Mould |
|---|---|---|
| Target Volume & Life | 100,000 – 300,000 shots | 500,000 – 1,000,000+ shots |
| Cavity & Core Steel | P20H / 718H (Pre-hardened HRC 30–33) | German DIN 1.2738 / 1.2738HH (HRC 34–38) |
| Parting Structure | External or Semi-Internal Parting | Full Internal Parting (Zero visible seam on A-surface) |
| Hot Runner System | 6–8 Drop Open or Valve-Gate Manifold | 8–12 Drop Sequential Valve Gate (SVG) — Yudo / Synventive / HRSflow |
| Sliders & Lifters | Nitrided 718H + Bronze Graphite Wear Plates | Hardened 1.2344 (H13, HRC 48–52) + Self-Lubricating Guide Rails |
| Cooling Design | 3D Milled Baffle & Bubbler Circuits | 3D Conformal Cooling + Beryllium-Copper (BeCu) Inserts in Thick Ribs |
| Typical Resin | PP + EPDM, Unfilled PP | PP + EPDM-TD20 (20% Talc-Filled Impact Copolymer) |
| Press Tonnage | 1,800T – 2,400T | 2,400T – 3,200T |
| Cycle Time | 50 – 65 seconds | 40 – 50 seconds |
| T1 Sample Lead Time | 55 – 65 days | 65 – 80 days |
Bumper & Exterior Fascia Moulds We Build
Front Bumper Fascia Moulds
Complex multi-action tools integrating headlight washer cutouts, radar/PDC sensor brackets, tow-hook covers, and integrated lower splitter lips.
Rear Bumper & Diffuser Moulds
Single-piece rear fascias, step pads, dual-exhaust valence panels, and textured unpainted lower diffusers with crisp grain release.
Radiator Grille & Trim Moulds
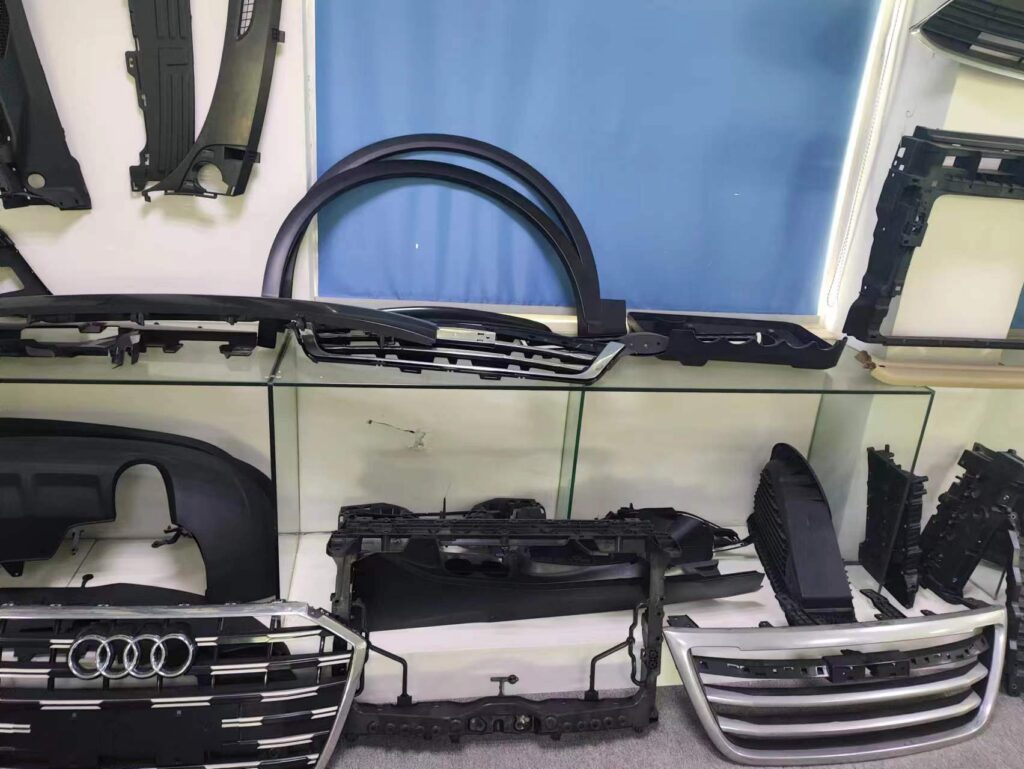
High-gloss piano-black ABS/ASA grilles, chrome-plating-grade mesh grilles, fog-light bezels, and wheel-arch fender flares — see our automotive plastic mold solutions.
How We Engineer Zero-Defect Bumper Tooling
1. Internal Parting & Complex Lifter Mechanics
A bumper’s wraparound ends and mounting flanges create deep undercuts in three axes. In an Internal Parting bumper mould, the main core and secondary rail-guided sliders move inward during the opening stroke, releasing the undercut flanges toward the inside of the bumper. All ejector pins, lifter witness lines, and parting seams sit exclusively on the B-side (inner surface), leaving the painted A-surface completely untouched.
2. SVG Sequential Gating & Anti-Sink Rib Rules
To prevent sink marks opposite mounting clips and licence-plate bosses, we enforce a strict rib-to-wall ratio of ≤ 0.5T (1.2–1.5 mm rib root on a 2.8 mm wall) during our free DFM analysis. Using Moldflow pressure-drop simulation, we time each SVG valve pin to open 0.1s after the melt front passes it — eliminating hesitation marks, air traps, and paint-revealing stress halos.


Cycle-Time ROI & 70-Day Tooling Program
Running a 2,500-ton injection press typically costs $90–$130/hour. Shaving just 8 seconds off a bumper cycle (from 53s down to 45s via BeCu inserts and optimized water-manifold zoning) increases output from 67 to 80 bumpers per hour. Over a 250,000-part production run, that 8-second reduction saves 555 press hours — over $55,000 in direct machine cost, paying back a huge portion of the mould investment. Compare your own numbers with our unit cost breakdown calculator.
Day 1–3: 24h Quote & DFM + Moldflow
We review your 3D CAD, check draft angles on textured grilles, simulate SVG valve-gate timing, and lock in the parting-line concept.
Day 4–15: 3D Tool Design & Steel Forging
Full 3D UG/NX assembly design sign-off while ultrasonic-tested DIN 1.2738 / 718H forged blocks are rough-milled and stress-relieved.
Day 16–50: 5-Axis CNC, Deep-Hole Drilling & EDM
High-speed 5-axis contour milling, deep-hole cooling channel drilling, mirror EDM on ribs, and plasma nitriding on all sliding lifters.
Day 51–62: Spotting Press Fitting & T1 Trial
Precision die-spotting on a 500T spotting press for 90%+ blue-lead shutoff contact, followed by T1 trial on our 1,800T–3,200T trial presses.
Day 63–70: Checking Fixture CMM & Export Shipment
Samples are verified on a dedicated 1:1 bumper checking fixture (gauge), followed by a 2-hour continuous dry-run video before sea/rail shipment.
Sourcing a Front or Rear Bumper Mould?
Send your 3D CAD (STEP/IGES/CATIA) or physical bumper sample. Our senior automotive tool engineers will return a free DFM report, SVG gate layout, and itemized quote within 24 hours.
- Internal & External Parting bumper tooling
- Full Moldflow warpage & SVG sequential gate simulation
- 1:1 Checking Fixture (Gauge) available with the tool
Automotive Bumper Mould FAQ
What is the difference between Internal Parting and External Parting in a bumper mould?
In a traditional external-parting bumper mould, the sliders split on the outer edge of the bumper, leaving a visible parting line that requires manual de-flashing before painting. An Internal Parting bumper mould uses complex rail-guided core pullers that move inward during mold opening, hiding all parting lines and lifter seams on the inner, non-visible flange of the bumper for a flawless Class-A exterior surface.
How much does a custom plastic car bumper mould cost in China?
An aftermarket (AM) bumper mould built in P20H/718H with external parting typically costs between USD 45,000 and USD 75,000. A full OEM Tier-1 production bumper mould built in German DIN 1.2738 with Internal Parting, an 8-to-12 drop Sequential Valve Gate (SVG) hot runner, and a 1:1 checking fixture ranges from USD 80,000 to USD 140,000+. Send your 3D file for an exact itemized quote within 24 hours.
How do you eliminate weld lines on a painted bumper fascia?
We use a Sequential Valve Gate (SVG) hot runner system (typically 8 to 12 nozzle drops). Instead of opening all gates at once — which traps air and creates knit lines where melt fronts meet — the center gates open first and outer wing gates open sequentially as the melt wave passes each pin, producing a single continuous flow front with zero visible weld lines.
What plastic material and shrinkage rate are used for car bumpers?
Most OEM bumpers are molded from modified polypropylene impact copolymer filled with 15%–20% EPDM rubber and 10%–20% talc (PP+EPDM-TD20, shrinkage ~0.9%–1.2%), which balances low-temperature impact toughness with dimensional stability and low thermal expansion (CLTE).
Do you also supply the 1:1 bumper checking fixture (inspection gauge)?
Yes. Because a flexible plastic bumper can deform under its own weight when measured on a flat table, we design and manufacture the 1:1 CNC aluminum/epoxy checking fixture alongside the mould to verify headlamp gap, fender flushness, and mounting-clip positions before shipping the tool.

